Article
Aseptic manufacturing: the most common audit findings
- WhenOctober 2026
- WhereMontreal, Quebec
- FormatArticle
- CategoryPublications and videos
Media fills that are too short, smoke studies in empty rooms, corrective actions closed without verification: seven typical findings in aseptic manufacturing, drawn from our audit checklist, and how to fix them before the inspection.
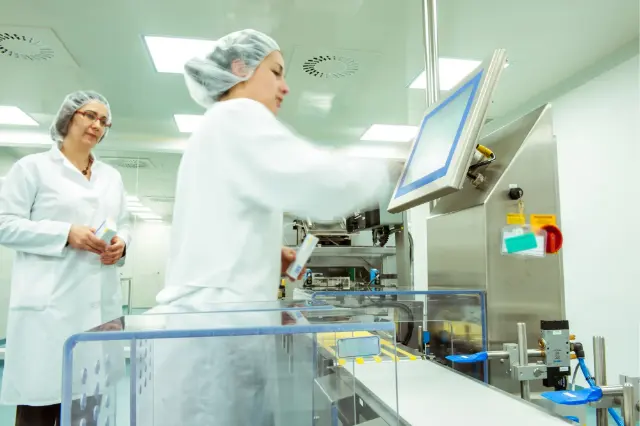
Since the revised EU GMP Annex 1 took effect in 2023, inspectors have been looking closely at how each sterile site controls contamination. Our aseptic manufacturing audit checklist covers 10 areas and 78 checkpoints. Here are seven findings that come up often across the industry, all rated critical or major.
Media fills that don’t reflect reality
An aseptic process simulation that is too short and leaves out the riskiest interventions proves very little. It must reproduce the worst case: the maximum duration, every planned intervention and the actual line speed, twice a year for each line and each shift.
A contamination control strategy gathering dust in a binder
Annex 1 requires a contamination control strategy. Too often, it is a document written once, never linked to real data and never reviewed after an incident. It needs an owner, must be based on risk management (ICH Q9) and should be reviewed after every event.
Smoke studies done in empty rooms
Watching airflow in an empty room does not show what happens during production. Smoke studies must be done under real operating conditions, with the riskiest interventions, recorded on video, then repeated after any layout change.
Trends no one is tracking
Reacting only when a limit is exceeded means reacting too late. Statistical trend analysis of environmental monitoring data catches drift before an excursion and triggers the investigation in time.
Water for injection with dead legs
Dead legs in the loop, a circulation temperature that is too low or haphazard endotoxin testing: water for injection must circulate continuously at high temperature, with no dead legs and with endotoxin monitoring at every point of use.
Cleaning limits chosen out of habit
A 10 ppm limit set “because that’s how it’s always been done” no longer holds up. Cleaning limits must be calculated from the permitted daily exposure (PDE or HBEL), with validated recovery and justified hold times.
Corrective actions closed without checking that they work
Retraining the operator as the only action, again and again, hides the real cause. A corrective and preventive action (CAPA) should be closed only after a root cause analysis and an effectiveness check.
What about over-compliance?
An audit doesn’t only look for what is missing. Our checklist also flags requirements that are exceeded for no reason, which cost a lot without adding anything to product safety. A good quality system is also a right-sized one.
Preparing for an inspection by the FDA, Health Canada or a European authority? Our team can audit your site against this checklist and give you a dashboard for each area, along with the corrective action plan.